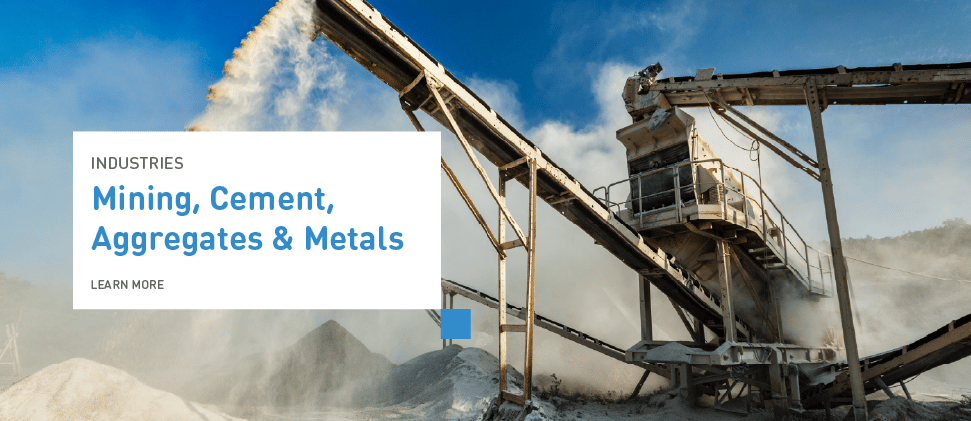
Walk into a remote pit operation running crushers, conveyors, and dewatering pumps off a single packaged mine skid, and you'll find the equipment doing exactly what it was specified to do on day one. Come back 18 months later, and something has changed. Trips are more frequent. Thermal alarms show up on the night shift. A contactor that ran clean for a year now chatters under load. The skid is still running — but the maintenance burden is climbing, and the root causes aren't always where the troubleshooting starts.
Packaged mine skid failures in remote mining operations rarely announce themselves with a single catastrophic event. They accumulate. Dust infiltrates enclosures. Thermal cycling loosens connections. Vibration from nearby crushers fatigues components that were never rated for the actual duty cycle. And because these skids often sit hundreds of kilometers from the nearest service depot, every unplanned outage carries a cost multiplier in mobilization, lost production, and emergency freight that fixed-plant facilities never face.
This guide breaks down the primary failure modes that shorten packaged mine skid life in remote pit environments, explains the engineering decisions that separate reliable equipment from premature replacements, and lays out a practical framework for specification, maintenance, and retrofit planning. Benshaw builds mine skids for exactly these conditions, backed by 40+ years of applied motor control expertise and hundreds of completed mining projects worldwide.
Why Packaged Mine Skids Fail Prematurely in Remote Pit Operations
Remote pit environments impose a combination of stresses that general-purpose motor control equipment was never designed to handle simultaneously. Understanding these failure drivers is the first step toward specifying equipment that actually survives the duty cycle.
Dust and Particulate Ingress
Calcite powder, bauxite fines, fine silica, iron ore fines: the airborne particulate at a remote pit operation does more than coat surfaces. It works into enclosure seals, clogs cooling pathways, and creates conductive bridges across insulation barriers. A mine skid in a NEMA 3R enclosure might pass inspection in a warehouse, but NEMA 3R is not rated against windblown dust, and six months on a pit bench in Australia or Chile tells a different story. Dust-heavy sites call for dust-tight construction: NEMA 4, 4X, or 12 in North America, or IP5X/IP6X under IEC 60529, the rating system most Australian and South American sites specify against.
Dust accumulation on heat sinks and fans reduces thermal dissipation. Internal temperatures climb. Soft starters and drives derate — or trip outright on thermal faults, and the maintenance team adds "blow out the skid" to an already overloaded weekly schedule. According to North American Mining Magazine (2025), abrasive dust and fine particulates infiltrate motor frames and cause overheating, excessive wear, and reduced efficiency by damaging bearings, seals, and fan systems.
Thermal Cycling and Connection Degradation
Daily temperatures at remote pit sites routinely swing 20–30 °C (36–54 °F) from daytime highs to overnight lows. With each cycle, bus bars, terminations, and bolted connections expand and contract, and because different metals move at different rates, connections between them gradually work loose.
Connections that torqued correctly at commissioning loosen over hundreds of thermal cycles — creating hot spots that accelerate insulation degradation. These hot spots don't show up on a standard visual inspection. They require thermal imaging or acoustic monitoring to detect, ideally through infrared viewing windows so connections can be scanned without opening energized medium-voltage compartments and exposing technicians to arc-flash risk. By the time these hot spots cause a fault, the damage has often spread to adjacent components.
Vibration from Adjacent Equipment
Mine skids rarely operate in isolation. They sit on concrete pads or steel frames adjacent to crushers, screens, and conveyors that generate persistent mechanical vibration. That vibration transmits through the mounting structure into the electrical enclosure.
Over time, vibration fatigues solder joints on circuit boards, loosens terminal screws, and accelerates bearing wear in cooling fans. The failure mode is gradual — nuisance trips increase in frequency, intermittent faults appear and disappear. By the time the root cause is identified, the cumulative damage has shortened the remaining useful life of multiple components.
Power Quality at Remote Sites
Remote pit operations frequently draw power from long distribution lines, portable generators, or dedicated substations that serve fluctuating loads. Voltage sags during large motor starts, phase imbalance from uneven loading, and harmonic distortion from adjacent VFD installations all stress motor control equipment in ways that controlled factory environments never replicate.
A soft starter on the skid’s low-voltage side, commissioned at a stable 480V, behaves differently when the bus regularly sags 15 to 20 percent during an across-the-line crusher start across the yard. Undervoltage protection trips. Motors draw more current to carry their load through the dip, and starts take longer, adding heat the protection settings were never tuned for. If the skid’s protection coordination wasn’t designed for the site’s actual power quality profile, or the system has changed since the study was done, the equipment is fighting conditions it was never configured for. A coordination study reflects one point in time; every addition or alteration moves the system further outside the parameters it was built around.
Engineered Motor Control: The Specification Decisions That Drive Mine Skid Reliability
The difference between a mine skid that delivers its full design life, often 15 to 20 years or more, and one that requires major intervention at 18 months often comes down to specification decisions made months before the equipment ships.
Enclosure Design and Environmental Rating
Enclosure selection goes beyond picking a NEMA rating from a catalog. For remote pit applications, the enclosure must account for dust particle size, ambient temperature range, altitude (which affects cooling capacity), and the specific chemicals present in the ore body.
Benshaw MVMS Series mine skid controls are built with customizable metal-enclosed construction rated up to 15 kV and 3000 A, with withstand ratings up to 50 kA. The enclosure design integrates disconnect switches, protection relays, and transformers in a configuration that maintains thermal management — even under dust exposure and temperature extremes. Built for it.
Thermal Management and Derating
Every soft starter and drive has a published thermal derating curve. Nameplate ratings are typically published at 40°C ambient; above that, capacity falls, often by 1 to 2 percent per degree. A device rated for 100 A continuous at 40°C might only deliver 85 A at 50°C, and less still with airflow restricted by dust. Altitude compounds the problem: thinner air carries away less heat, so derating typically begins above 1,000 meters, and many Andean operations sit at 3,000 to 4,500 meters.
Specifying equipment based on nameplate ratings at 40°C ambient — the standard catalog condition — ignores the reality of a mine skid that will operate at 50°C+ with partially blocked ventilation channels for months between maintenance intervals. The specification should account for worst-case ambient, altitude derating, and a realistic dust accumulation factor. Oversizing the thermal capacity of the skid's starters and drives by 15 to 25 percent costs less than a single unplanned shutdown at a remote site.
Motor Protection and Diagnostics Integration
A mine skid that starts and stops motors without monitoring what happens in between is an operational blind spot modern facilities should not accept. Motor protection requires current monitoring, thermal modeling, fault logging, and communication with the site's SCADA or distributed control system.
Benshaw mine skids integrate protection relays with LED status indicators, configurable power distribution, and communication interfaces. The LEDs give technicians an at-a-glance status read at the skid without opening the enclosure on a dusty pit bench, while the relays’ communications carry motor health data back to the control room, so many developing problems can be spotted without a site visit at all. Here's what's really at risk when that visibility is missing: undetected thermal trends escalate from nuisance alarms to winding failures, and by then, you're looking at a motor replacement instead of a relay adjustment.
Protection Coordination for Real Site Conditions
Protection coordination on a mine skid means more than setting overload and short-circuit trip points. It means coordinating upstream and downstream devices so that a fault on one motor isolates that circuit — without cascading across the entire skid.
This requires understanding the site's actual fault current levels, the impedance of the distribution cables, and the starting characteristics of every motor on the skid.
Service Planning for Remote Mine Skid Installations
Specifying reliable equipment is only half the equation. The other half is keeping it reliable once it's operating 500 kilometers from the nearest service center.
Maintenance Interval Planning Based on Actual Conditions
Standard maintenance intervals derived from catalog recommendations assume controlled environments. A mine skid on a remote pit bench operates under conditions that accelerate every wear mechanism: dust, heat, vibration, and power quality stress.
Effective maintenance planning starts with a site-specific assessment of these environmental factors and adjusts intervals accordingly. As Reliability Center Inc. documents, the same equipment failure repeated across multiple sites often traces back to systemic conditions that standard maintenance intervals were never calibrated for. Thermal imaging of connections, insulation resistance testing, and protection relay event log reviews should occur at frequencies driven by field conditions, not catalog defaults.
Spare Parts Strategy and Lead Time Management
When a critical contactor or protection relay fails at a remote site, the cost isn't the part — it's the downtime while the part ships. For remote mine skid installations, a strategic spare parts inventory is a reliability investment, not a procurement expense.
Benshaw maintains the industry's largest inventory of packaged starters and drives, and supports both Benshaw equipment and third-party motor control systems with service, repairs, retrofits, and warranty support. Your spare parts strategy can draw from a supply chain built for industrial lead times. Benshaw also offers a two-year overload relay guarantee, giving your team extended coverage on a component that takes significant abuse in mining duty cycles.
Retrofit and Modernization Planning
Remote mine skids age faster than equivalent equipment in fixed-plant environments. Planning for retrofit before the skid reaches end-of-life avoids the scramble of emergency replacement — on the failure's schedule, not yours — during a production-critical period.
Benshaw supports practical retrofit upgrades that preserve your existing motors and infrastructure while replacing aging control components with current-generation starters, drives, and protection devices. This approach extends the installation's life without requiring a full skid replacement, keeping capital costs manageable and minimizing the outage window.
What to Specify When Ordering a Packaged Mine Skid
Use this framework when developing specifications for a new mine skid or evaluating whether an existing installation needs attention. Each item addresses a failure mode covered in this guide.
| Specification Area | What to Specify | Why It Matters |
|---|---|---|
| Enclosure rating | Dust-tight rating (NEMA 4/4X/12 or IP5X/IP6X) matched to the site’s actual dust and moisture conditions, not a generic "outdoor" classification | Prevents premature dust ingress and insulation bridging |
| Thermal capacity | Derate all components to the manufacturer’s curves for worst-case site ambient temperature and altitude (typically 15–25% above nameplate) | Equipment rated only for standard conditions runs hotter than designed at the site, shortening its service life and increasing nuisance trips. |
| Vibration isolation | Anti-vibration mounting for the electrical enclosure, separate from the structural skid frame | Reduces connection fatigue, board cracking, and fan bearing wear |
| Protection coordination | Site-specific fault study with actual cable impedances and motor starting profiles | Prevents nuisance cascade trips and ensures selective fault isolation |
| Diagnostics and communications | SCADA-ready protection relays with event logging and remote access capability | Enables condition-based maintenance and reduces unnecessary site visits |
| Spare parts coverage | Critical spares inventory based on MTBF analysis of site-specific failure modes | Cuts downtime from weeks to hours when a component fails at a remote site |
Differentiating Reliable Equipment from Marketing Claims
When evaluating packaged mine skid suppliers, the specification sheet only tells part of the story. The questions below separate verified performance from catalog promises.
Is the equipment tested to relevant industry standards, or merely designed in accordance with them? Tested means a documented, witnessed validation process. "Designed in accordance with" means nothing verifiable. Ask for test reports.
Does the supplier perform site-specific protection coordination? Generic trip settings applied across all installations indicate a one-size-fits-all approach. Your site's fault currents, cable lengths, and motor characteristics are unique. The protection scheme should reflect that.
What is the supplier's service capability at your site's location? A mine skid installed in a remote pit in Nevada, Western Australia, or northern Chile needs a service model that accounts for distance. Benshaw operates globally with factory-trained technicians and a supply chain built for mining lead times.
Does the equipment integrate with your existing control infrastructure? A mine skid that can't communicate with your plant's SCADA system or historian creates a data gap your reliability team can't afford. Benshaw motor control equipment integrates with standard industrial communication protocols, feeding motor health data into your existing monitoring and predictive maintenance systems.
Frequently Asked Questions
What causes packaged mine skids to fail prematurely in remote operations?
The primary failure drivers are dust ingress that degrades insulation and clogs cooling paths, thermal cycling that loosens connections over hundreds of temperature swings, persistent vibration from adjacent crushers and conveyors, and poor electrical supply quality at remote distribution points. These factors compound each other, accelerating wear beyond what standard-rated equipment can handle.
How does Benshaw design mine skids for harsh mining environments?
Benshaw MVMS Series mine skid controls use customizable metal-enclosed construction rated up to 15 kV and 3000 A, with withstand ratings up to 50 kA. Each skid integrates disconnect switches, protection relays, transformers, and configurable power distribution in an enclosure designed for operation under dust, vibration, and temperature extremes. Protection coordination is performed using site-specific fault data during the design phase.
What maintenance practices extend mine skid life at remote sites?
Adjust maintenance intervals based on actual site conditions rather than catalog defaults. Perform thermal imaging of connections and bus bars at regular intervals. Review protection relay event logs for trending fault patterns. Maintain a site-specific critical spares inventory based on mean time between failure analysis for components exposed to your particular environmental stresses.
When should a mine skid be retrofitted rather than replaced?
Retrofit makes sense when the skid's structural frame and power distribution remain sound but the motor control components (starters, drives, protection relays) have reached end-of-life or can no longer be supported with spare parts. Benshaw supports retrofit upgrades that preserve existing motors and infrastructure while replacing aging control equipment with current-generation devices, keeping capital costs controlled.
How do Benshaw mine skids integrate with SCADA and plant control systems?
Benshaw mine skids include protection relays with event logging, LED status indication, and communication interfaces compatible with standard industrial protocols. Motor health data, fault records, and operating parameters feed into your site's SCADA, historian, or predictive maintenance system, with a protocol gateway added only where your network requires one.
What questions should engineers ask suppliers when specifying mine skid equipment?
Ask whether the equipment has been tested to relevant standards or merely designed in accordance with them. Confirm that protection coordination uses your site's actual fault current data and cable impedances. Verify the supplier's service capability and lead times for your specific location. Check that the equipment supports communication with your existing control infrastructure. The conversation is worth having before the failure forces it.